Non-woven Fabric Explained: Types, GSM and Applications

Non-woven fabric is the one material category where the weight number on the spec sheet carries almost the entire meaning. Woven buyers talk about thread count and weave; non-woven buyers talk about grams per square metre, because there is no yarn and no weave to describe.
That makes GSM the most critical number in a non-woven purchase order — and the one most often under-specified. This guide sets out the five main production routes, how they differ in ways that matter at the converting machine and in the hand, how GSM maps to real applications, and the measurement and compliance points that decide whether a delivery is accepted.
How to read the figures in this guide
Standard – basis weight and thickness have published test methods (the ISO 9073 series, EDANA WSP methods, ASTM D1777) that you can cite in a contract. Convention – the GSM ranges shown against each application are widely used industry practice, not standardised values, and they overlap between producers. Verify required – fibre diameter, strength and barrier figures depend on the line, the polymer and the finish, so confirm them on a test report for the specific fabric and lot you are buying.
Three tiers of confidence:
- Standard — a published test method you can name on a purchase order.
- Convention — typical industry ranges. A starting point, not a guarantee.
- Verify required — line- and lot-dependent; confirm on a test report.
What non-woven means
A non-woven is a sheet made directly from fibre, bonded by mechanical, thermal or chemical means, without passing through yarn or weaving. Fibre in, fabric out, in one continuous line. That is why the category is cheap at volume and why it behaves so differently from a woven cloth at the same weight: there is no interlaced structure to distribute load, so the bond does the work.
Two consequences follow. First, non-wovens are anisotropic or isotropic depending on how the web was laid — a property you can specify, and one that matters when a fabric feeds through a converting line. Second, because there is no yarn, GSM is the practical measure of density, and it is what both sides of a negotiation will actually quote.
The five production routes
Each route produces a fabric with a recognisable signature, and the choice is usually settled by the application rather than by price.
| Route | How it is bonded | Fibre | Hand and character | Signature use |
|---|---|---|---|---|
| Spunbond | Thermal calendering of continuous filaments | Continuous PP or PET filaments, roughly 15–35 µm | Crisp, strong for its weight, visible bond pattern | Bag bodies, coverstock, gown outer layers, crop covers, furniture and mattress substrates |
| Meltblown | Self-bonding under high-velocity hot air | Ultrafine filaments, roughly 0.5–5 µm | Soft but fragile alone; the filtration layer | Respirator filter media, HVAC filters, mask mid-layers, oil sorbents |
| Spunlace | High-pressure water jets entangle the web | Staple fibre — viscose, polyester, cotton, lyocell and blends | Soft, cloth-like, low-linting, absorbent with cellulose | Wet wipes, facial towels, cosmetic pads, medical dressings |
| Needlepunched | Barbed needles mechanically interlock a carded web | Staple polyester, polypropylene, wool or recycled blends | Thick, felt-like, dimensionally stable, the heaviest of the group | Geotextiles, automotive liners, filter felts, synthetic leather substrates |
| Airlaid | Short fibre laid from an air stream, then bonded | Fluff pulp, sometimes with synthetic fibre | Bulky, lofty, highly absorbent, softer than paper at equal weight | Absorbent cores, premium napkins, food-tray pads, underpads |
A quick rule of thumb that holds up in most sourcing conversations: anything touching skin repeatedly is specified as spunlace; anything that must cover, carry or protect at the lowest cost per square metre is specified as spunbond. Spunlace costs more because staple fibre is dearer and hydroentangling plus drying takes energy.
Spunbond, meltblown and SMS side by side
| Property | Spunbond | Meltblown | Spunlace | SMS |
|---|---|---|---|---|
| Fibre diameter | 15–35 µm | 0.5–5 µm | Fibre-dependent | Composite |
| Bonding | Thermal / calender | Self-bonding airflow | Water jets | Layered |
| Tensile strength | High | Low | Medium | High |
| Filtration / barrier | Low | Highest | Low | High |
| Softness | Coarse | Soft but fragile | Most cloth-like | Medium |
| Relative cost | Low | Medium | Medium to high | Medium |
SMS — spunbond, meltblown, spunbond — is the composite at the centre of medical and protective applications: two strength layers wrapping a barrier layer. Variants such as SMMS and SSMMS tune the ratio of strength to barrier by adding layers.
The commercial point most buyers miss: SMMS delivers a better barrier-to-weight ratio than SMS, because the double meltblown layer filters more at equal or lower total GSM. In practice a 40 gsm SMMS can outperform a 50 gsm SMS on the critical barrier specification while costing less per metre. If you are comparing quotations on GSM alone, you are comparing the wrong thing.
GSM selection by application
GSM — grams per square metre — is the weight of a one-square-metre sample. The table below gives the ranges most commonly specified against each application. These are conventional practice rather than standard values, and they are the starting point for a conversation with a mill, not a substitute for one.
| Application | GSM range | Type | Critical property |
|---|---|---|---|
| Coverstock, baby care | 12–18 | Spunbond PP | Softness, liquid pass-through |
| Coverstock, feminine care | 15–22 | Spunbond PP | Skin comfort, moisture wicking |
| Wet wipe substrate | 30–50 | Spunlace / spunbond | Wet strength, softness |
| Isolation gown | 25–40 | SMS | Barrier plus breathability |
| Surgical gown | 35–50 | SMS | Liquid barrier plus drape |
| Surgical drape | 45–70 | SMMS | High liquid resistance |
| Light coverall, cleanroom | 30–40 | Spunbond | Particulate barrier, strength |
| Heavy coverall, chemical | 50–70 | SMS | Chemical resistance |
| Apparel interlining | 25–50 | Spunbond | Shape retention, hand feel |
| Agricultural frost cover | 15–30 | Spunbond | Light transmission plus strength |
| Mattress and furniture cover | 60–80 | Spunbond | Shape stability, durability |
| Shopping and tote bags | 60–120 | Spunbond / laminated | Tensile and seam strength, print surface |
| Geotextile, road | 100–200+ | Spunbond / needlepunched | Load bearing, drainage |
Note the direction of the failure risk. Going too heavy on a hygiene coverstock produces something rigid and plastic-like that a brand owner will reject on feel; going too light causes web formation problems and tensile failure on a converting line running at speed. The window is narrow and it is application-specific.
Thickness: the number that needs a pressure next to it
Non-wovens are compressible, so thickness is meaningless without the pressure it was measured at. The same fabric measured at 0.5 kPa and at 4.14 kPa gives materially different results. Thickness is defined as the perpendicular distance between the two faces under a specified applied pressure — not at zero load.
The relevant methods are ISO 9073-2 for non-woven thickness and ASTM D1777 for textile thickness generally; basis weight is covered by ISO 9073-1 and by the corresponding EDANA WSP method. Always state the pressure alongside a thickness requirement.
| Type | Typical thickness | Typical basis weight |
|---|---|---|
| Meltblown | 0.06–0.10 mm | 15–40 gsm |
| Spunbond | 0.10–0.50 mm | 10–150 gsm |
| Needlepunched geotextile | 0.50–8.0 mm | 80–1,200 gsm |
| Insulation batting | Over 10 mm | Over 1,000 gsm |
Thickness, basis weight and density are related but distinct. Two fabrics of identical thickness and different fibre denier will filter, insulate or reinforce at entirely different levels — which is why thickness results always need the construction stated alongside them.
Fibre choice: polypropylene versus polyester
| Polymer | Behaviour | Where it wins | Where it loses |
|---|---|---|---|
| Polypropylene (PP) | Lower melting point, runs faster, lower density, inherently hydrophobic | Hygiene, medical disposables, the bulk of spunbond and meltblown | Lower heat tolerance and lower UV resistance than PET |
| Polyester (PET) | Higher melting point, better UV and heat resistance, stronger | Geotextiles, roofing and construction, automotive, technical applications | Costs more and runs slower than PP |
The choice is usually settled by the service environment. A fabric that will sit outdoors for years is a PET question; a fabric that will be worn once and discarded is a PP question.
Finishes that turn a substrate into a product
Most non-woven performance attributes buyers care about are applied rather than inherent:
- Hydrophilic finish — untreated polypropylene repels water; a finish is what makes a coverstock pass liquid through. Essential and easy to forget on a specification.
- Antistatic — needed where the fabric runs at speed or where dust attraction matters.
- Flame retardant — required for many automotive, construction and protective applications, and subject to the applicable product standard for the end use.
- UV stabilisation — required for agricultural and geotextile applications with outdoor exposure.
- Antibacterial and softness finishes — common in wipes and personal care.
- Print and lamination surface treatment — decides whether a bag fabric takes ink and whether a laminate bonds.
Specify the finish explicitly and state how its durability will be assessed, because a finish that washes off or migrates has a defined service life rather than an indefinite one.
Applications by industry
| Industry | What it buys | Typical route |
|---|---|---|
| Hygiene | Coverstock, acquisition layers, absorbent cores | Spunbond, airlaid |
| Medical and protective | Gowns, drapes, masks, respirator media | SMS / SMMS, meltblown |
| Wipes | Baby, personal care, household, industrial | Spunlace, airlaid, spunbond |
| Apparel | Interlining, disposable protective workwear | Spunbond |
| Packaging and retail | Reusable bags, wrapping, protective covers | Spunbond, laminated spunbond |
| Construction and geotextiles | Separation, filtration, drainage, reinforcement, roofing | Needlepunched, PET spunbond |
| Automotive | Trunk liners, carpet backing, insulation, filter media | Needlepunched, meltblown |
| Agriculture | Frost and crop covers, weed control | UV-stabilised spunbond |
Testing and compliance
The properties worth specifying, and how they are normally measured:
- Basis weight — ISO 9073-1, or the corresponding EDANA WSP method.
- Thickness — ISO 9073-2 or ASTM D1777, with the applied pressure stated.
- Tensile strength and elongation — the ISO 9073 series covers non-woven tensile testing; state machine and cross-direction separately, because most non-wovens are not equal in both.
- Barrier and filtration performance — tested to the standard appropriate to the end use, which for respiratory and medical products is a product standard rather than a fabric standard.
- Chemical compliance — REACH applies to articles placed on the EU market; OEKO-TEX STANDARD 100 is the common limit-value framework for textile articles, with Class I the level for babies and toddlers.
- Packaging — non-woven packaging placed on the EU market is subject to the Packaging and Packaging Waste Regulation (Regulation (EU) 2025/40), which sets recyclability and recycled-content requirements with staged application dates. Confirm which obligations apply to your format.
Confirm the current version and scope of each standard and instrument before citing it in a contract; this guide names the methods normally used and is not a substitute for the published documents or for legal advice.
Buyer checklist
Write these into the specification:
- Production route — spunbond, meltblown, spunlace, needlepunched, airlaid, or a stated composite such as SMS or SMMS.
- Polymer — PP or PET, and whether recycled content is required and to what certification.
- GSM with tolerance — and the test method.
- Machine and cross-direction strength — stated separately, with methods.
- Thickness with the measurement pressure, if thickness is specified at all.
- Finish — hydrophilic, antistatic, FR, UV, antibacterial — with a durability requirement.
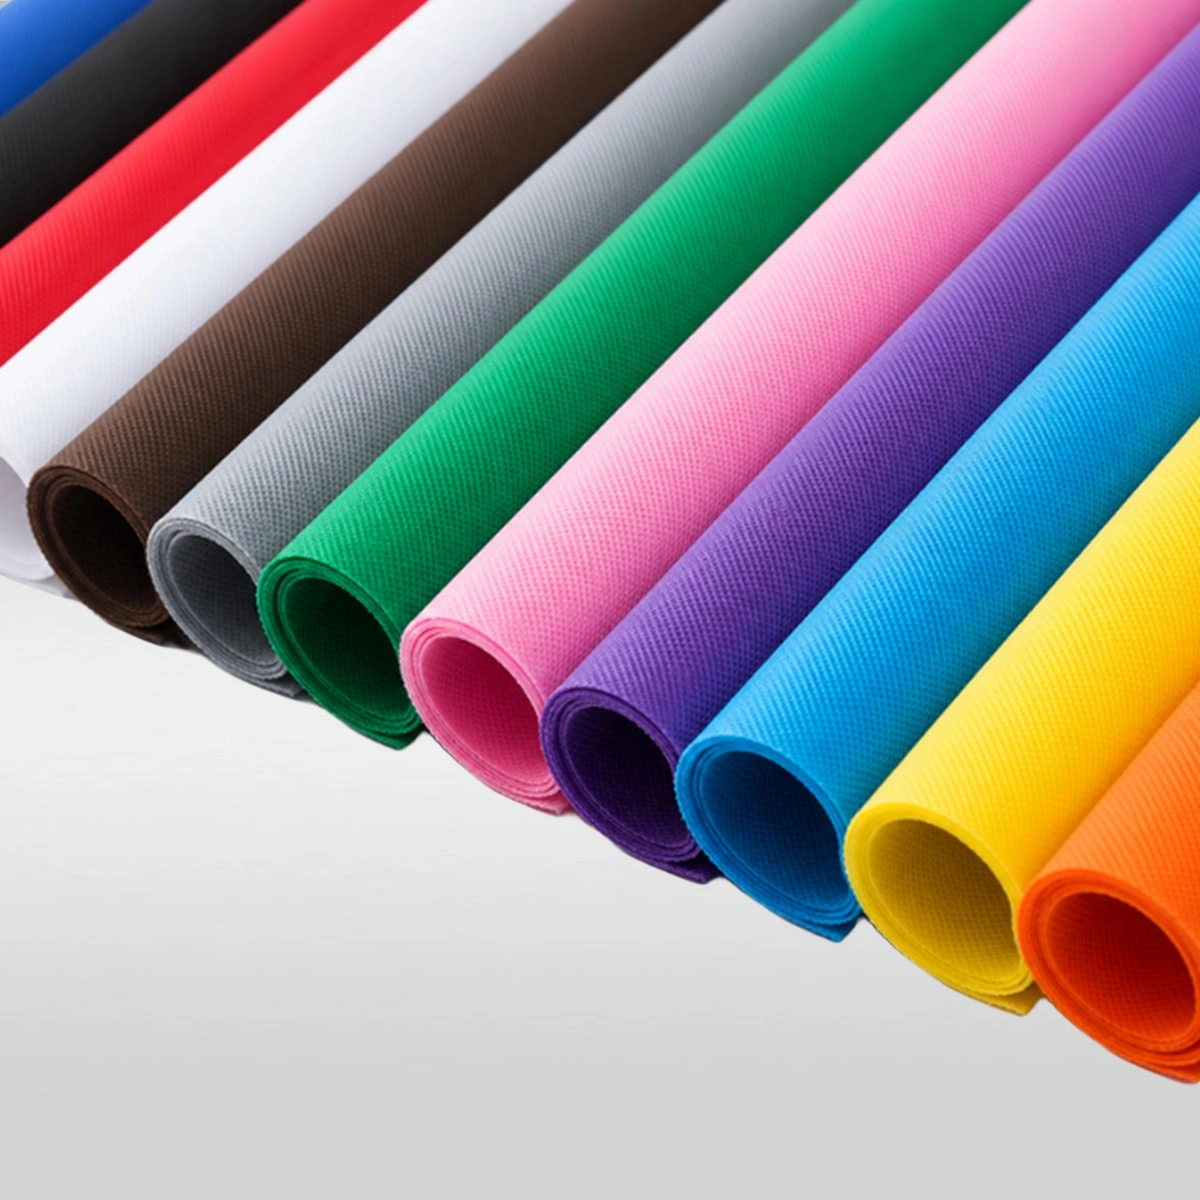
- Colour and shade standard, with tolerance, if the fabric is dyed or pigmented.
- Roll specification — width, roll length, core, splice policy and maximum splices per roll. Splices matter on a high-speed line.
- Barrier or filtration requirement, tested to the product standard for the end use.
- Retained sample — a labelled sample from each lot, with the test report attached.
Frequently asked questions
What is the difference between spunbond and spunlace?
Bonding, and everything that follows from it. Spunbond is bonded with heat from continuous filaments and behaves like a strong, papery sheet; spunlace is bonded with high-pressure water jets from staple fibre and behaves like cloth. Spunlace is softer and more absorbent, spunbond is stronger and cheaper at the same weight. Anything touching skin repeatedly is normally spunlace.
What does SMS mean?
Spunbond–meltblown–spunbond: two strength layers with a filtration layer between them. It combines the durability of spunbond with the barrier of meltblown in one fabric, which is why it dominates surgical gowns, drapes and sterile packaging. SMMS adds a second meltblown layer for a better barrier-to-weight ratio.
Is a higher GSM always better?
No. Each application has a window. Too heavy on a hygiene coverstock makes it rigid and plastic-like; too light causes web and tensile failures on a converting line. In barrier applications, a better-constructed lighter fabric — SMMS rather than SMS — can outperform a heavier one, so compare barrier performance at weight rather than weight alone.
Why do two thickness measurements of the same fabric disagree?
Because non-wovens compress. Thickness is defined at a specified applied pressure, and the same fabric measured at 0.5 kPa and at 4.14 kPa gives different answers. Always state the pressure with the requirement and specify the method — ISO 9073-2 or ASTM D1777.
Polypropylene or polyester?
Polypropylene for disposables, hygiene and medical — it runs faster and costs less. Polyester for anything durable, outdoor or exposed to heat: geotextiles, roofing, automotive, technical textiles. The decision usually turns on service environment rather than on price.
Why does water bead on my polypropylene non-woven?
Because polypropylene is inherently hydrophobic. If you need liquid to pass through — a coverstock, a wipe, an absorbent layer — you need a hydrophilic finish specified explicitly. This is the most commonly omitted line on a non-woven specification.
Can I specify recycled content?
Yes, and increasingly buyers do, but specify the documentation as well as the percentage. Ask which third-party scheme certifies the claim and request the corresponding transaction or scope certificate, rather than accepting the word “recycled” unsupported.
Production routes, polymer behaviour and test methods in this guide follow published standards and widely used industry practice; the GSM ranges against each application are conventional starting points rather than standard values. Confirm basis weight, strength, barrier performance and finish durability on a test report for the specific fabric and lot before ordering at volume.
Browse our range: Interfacing · Packaging Supplies · Shopping Bags · Reflective Materials
Share This Article
Follow Us
Blog Categories
Latest Articles
September 30, 2026
September 30, 2026
September 30, 2026